Precision Gear Racks: Ground vs Milled Series
How the five precision rack series differ — ground and milled, straight and helical, hardened and tempered — with pitch error figures and a selection order.
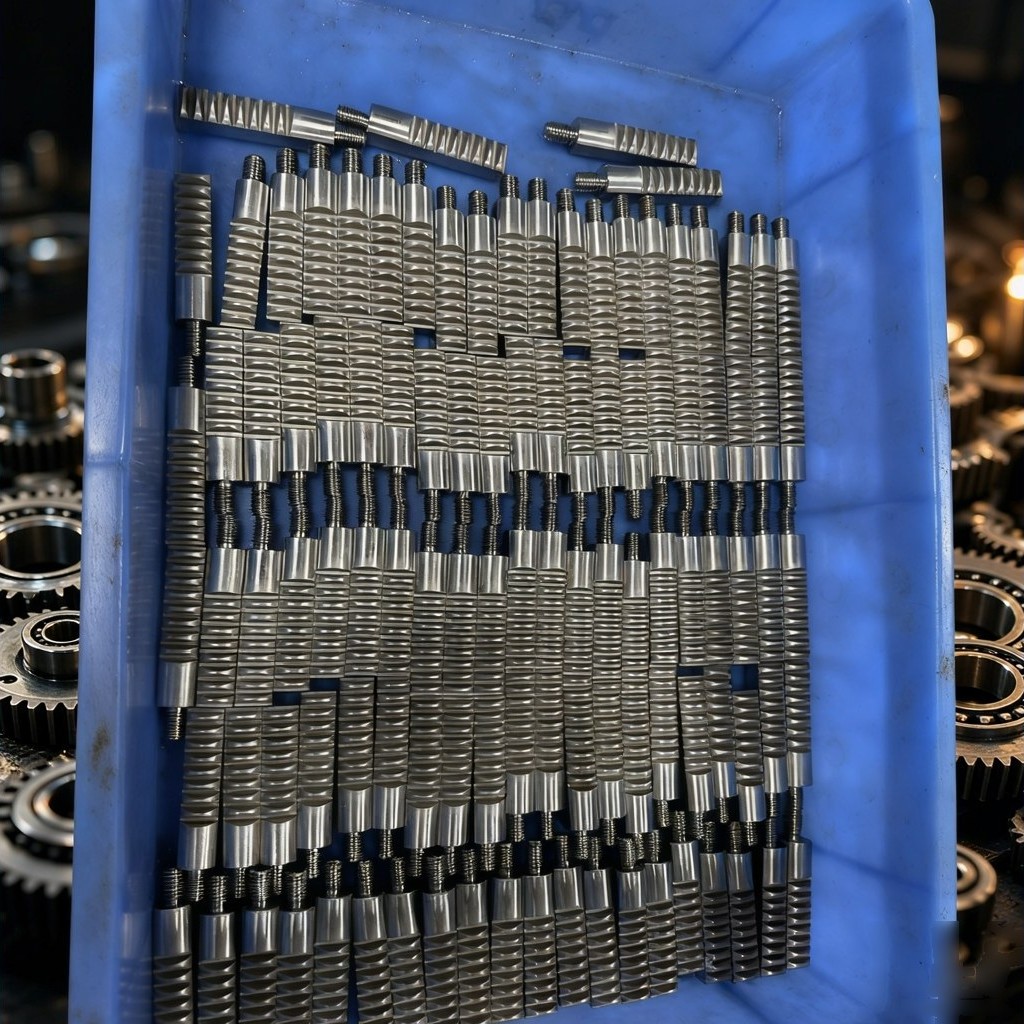
A rack turns rotation into travel, and it does so in a straight line. That single geometric fact drives every specification on the drawing. A gear closes on itself, so the error of one tooth is shared among all of them; a rack keeps going, so the error of one tooth is carried forward and added to the next. Rack accuracy is therefore quoted as cumulative pitch error over a distance — typically per 1000 mm — not as a single tooth measurement.
The precision rack range is built from two decisions and one material condition: how the flank is made (ground or milled), whether the tooth is straight or helical, and whether the part is hardened or left tempered for later machining. Those combinations produce five series, and the differences between them are measurable rather than promotional.
What the designation actually contains
A callout such as DIN 6h25 carries two separate pieces of information. The leading number is the accuracy grade. The letter and number that follow belong to the DIN 3967 system of tooth thickness allowances and tolerances, where the trailing figure is the tooth thickness tolerance in micrometres — 25 in this case. Neither of those describes how far the axis will drift over a metre of travel.
Cumulative pitch error is the parameter that governs position along the rack, and it is the one that shows up as a positioning complaint. On the ground series it is held to 0.036 mm per 1000 mm. On the milled series it is 0.08 mm per 1000 mm for the tempered variant and 0.13 mm per 1000 mm for the hardened and helical milled variants. A drawing that specifies only the tooth thickness class leaves the more consequential number undefined, and the gap surfaces at assembly when the backlash does not match the calculation.
The two ground series
Both ground series reach DIN 6h25 with 0.036 mm total pitch error per 1000 mm, in S45C (C45) medium carbon steel at a 20° pressure angle, induction hardened to HRC 48–52, with ground flanks and all four sides ground. Modules cover 1, 1.5, 2, 3, 4, 5, 6, 8, 10 and 12 in standard lengths of 500 mm and 1000 mm.
Four-sided grinding is not a cosmetic addition. A rack bolts down against a datum face, and if the bottom and reference side are left as-machined the installer closes the gap with shims. The accuracy verified in the inspection room is then partly spent on the mounting, and two identical racks can behave differently on two different machines because the installation differed. Grinding the sides is what allows the measured value to survive being bolted down.
The choice between straight and helical at this accuracy level is a question of contact, not of class. The helical version is cut right-hand at 19°31'42". A higher contact ratio means more teeth share the load at any instant, load per tooth falls, each tooth enters and leaves contact more gradually, and a fast axis runs with less noise. The trade is axial thrust, which the bearings and guideways must absorb; a rack cannot resist it. Straight ground racks produce no axial force, keep the surrounding structure simple, and remain the common choice for X and Y positioning axes.
The three milled series
Straight milled, hardened runs to DIN 10e27 with 0.13 mm per 1000 mm, S45C, milled flanks, induction hardened HRC 48–52, modules 1 to 10. Surface hardness is present; the accuracy is deliberately relaxed. General power transmission, conveyor drives and gantry lifting live comfortably inside that envelope.
Straight milled, tempered runs to DIN 8e27 with 0.08 mm per 1000 mm, tempered to HRC 18–20 with flanks left unhardened. This series exists because hardened racks are awkward to modify after delivery. Drilling, pocket milling and tapping in HRC 48–52 material is slow, and a customer who needs holes positioned from the machine at installation cannot produce them in a hardened part without a second setup elsewhere. In the tempered state the rack is fitted, marked and drilled on site. For light-duty mechanisms and non-standard drives requiring secondary operations, that flexibility is worth more than the hardness.
Helical milled runs to DIN 10e27 with 0.13 mm per 1000 mm, right-hand 19°31'42", hardened HRC 48–52, modules 1 to 10. It costs no more accuracy than the straight milled version and delivers the quieter running of helical contact, which suits axes fast enough for noise to be noticed but not demanding enough to justify grinding.
Choosing between them
Work through three questions in order.
Accuracy first. If cumulative error must stay inside 0.05 mm per 1000 mm, only the ground series qualifies. If 0.1 mm per metre is acceptable, milling meets the requirement and the additional cost returns nothing the application can use.
Then stroke and joints. Racks join into any length using pitch-matched joints and locating pins. A three-metre axis assembled from one-metre bars contains two joints, and each joint is a point where accumulated accuracy can slip. The longer the axis and the more joints it carries, the stronger the argument for stepping up a class instead of accepting the lower one.
Then what happens after delivery. Holes, slots, keyways and pins to be added in-house point to the tempered series. Bolt-on-and-forget points to hardened.
Stock and inspection
Standard straight racks are held in modules m1, m1.25, m1.5, m2, m2.5, m3, m3.5, m4 and m5, in sections from 10×10 mm to 50×50 mm and lengths of 1 m, 1.5 m, 2 m and 3 m, with optional drilling, quenching, blackening, zinc plating, chrome plating and grey finishing. Stock answers a lead-time question rather than an accuracy question: that tier runs at conventional accuracy, and a DIN 6h25 requirement still means a grinding order.
Verification suits the parameter being claimed. A gear measuring center reports profile, lead and pitch deviations against the specified class; hardness and roughness checks confirm that heat treatment and finishing did what the drawing asked; a meshing check confirms contact pattern and backlash behaviour in the assembly rather than on the bench.
Racks are machined to drawing, with module, pressure angle, helix angle, bar length, joint positions, material and heat treatment taken from the print. More on tooth geometry and the drawing details that decide manufacturability is in the rack product page.