

Spur and Helical Gears Machined to Customer Drawing
Spur and helical gears machined to the customer drawing, with tooth data, material and accuracy class taken from the drawing.
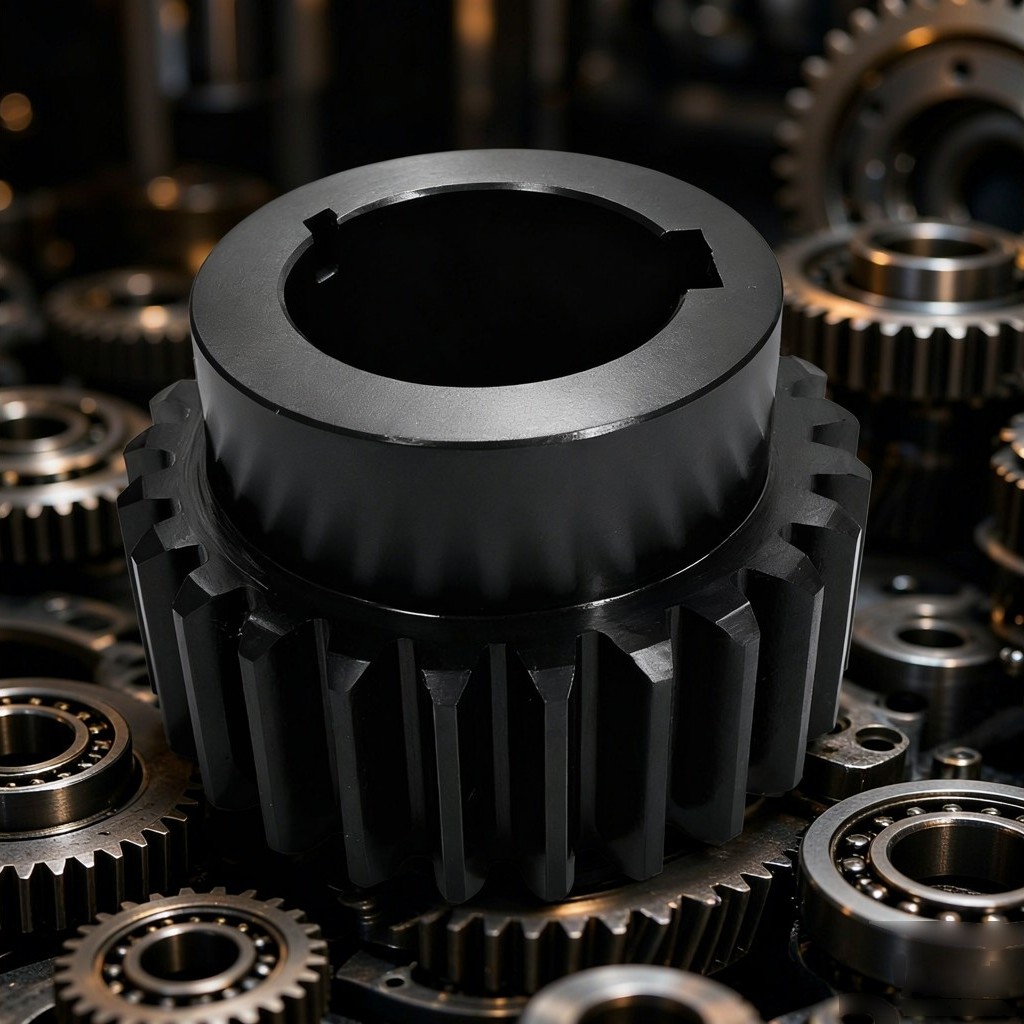
PinyiGear machines spur and helical gears to the customer drawing. Tooth count, module, pressure angle, helix angle and hand, face width, bore and keyway, material and heat treatment all come from the drawing, because the gear is made for a specific assembly rather than picked from a range.
That single fact decides how the job is run: there is no catalogue part to fall back on, no standard blank to modify, and no tolerance that can be waved through as “close enough”. The drawing is the specification, and the first useful thing we can do with it is read it carefully enough to find what it leaves open.
Where the drawing decides the part
- Tooth data — number of teeth, module, pressure angle, helix angle and hand, profile shift where the drawing specifies one
- Body data — outside diameter, face width, bore, keyway or spline, hub and web dimensions
- Quality data — the accuracy class, and the datum faces against which the tooth is measured
- Treatment data — steel grade, heat treatment, and the hardness range expected after it
When part of this is missing from the drawing, we ask before quoting. A gear quoted on guessed tooth data is a gear that has to be made twice.
The datum question comes up more often than people expect. A gear measured from the bore and a gear measured from the pitch circle are two different acceptance criteria for the same part; if the drawing does not say which one governs, the inspection report at the end will not agree with the drawing at the start.
Gear types we machine
- Spur gears, external and internal
- Helical gears, right hand and left hand
- Gear shafts, with the teeth cut on the shaft body
- Gear blanks and rough-cut parts for further processing by the customer
- Profile-shifted variants, where the drawing gives the shift coefficient
- Paired sets, where the pinion and wheel are cut for a stated centre distance
Internal gearing and gear shafts are worth a note. Internal teeth are cut with a shaping cutter rather than a hob, so the tooling is specific to module and tooth count and the lead time is longer than for an external gear of the same size. Gear shafts need the teeth cut in the same setup family as the bearing journals, otherwise the runout between the tooth and the journals shows up as noise at speed.
How the job runs
The process route follows the accuracy class and the heat treatment, in that order. A gear that will be case-hardened after cutting needs enough stock left on the flank for the distortion to be ground away; a gear that is finished before heat treatment cannot be corrected afterwards.
- Blank preparation — turning, boring, facing, with the datum faces established here and protected through the rest of the route
- Tooth cutting — hobbing for external spur and helical teeth, shaping for internal teeth and for shoulders that block a hob
- Heat treatment — where the drawing calls for it, with the distortion allowance built into the cutting dimension
- Finishing — shaving for moderate classes on unhardened gears, grinding for hardened gears and for the tighter classes
- Inspection — tooth parameters, runout, and the features the drawing lists as critical
Which step carries the accuracy is the engineering decision. Hobbing alone holds the commercial range for most external gears; when the drawing asks for a class that hobbing cannot hold, the route gains a finishing step and the price gains the cost of it.
Accuracy classes and what they mean
Four systems appear in drawings we receive: ISO 1328, DIN 3962/3967, AGMA 2015 and GB/T 10095. They describe the same physical deviations with different grade numbering, and the numbering runs in opposite directions — DIN grade 1 is the tightest, AGMA grade 16 is the tightest.
| System | Tightest | Loosest in common use | Direction |
|---|---|---|---|
| DIN 3962 | 1 | 12 | Lower number = tighter |
| ISO 1328 | 1 | 12 | Lower number = tighter |
| AGMA 2015 | 16 | 6 | Higher number = tighter |
| GB/T 10095 | 1 | 12 | Lower number = tighter |
As a working range, ground gears come out at DIN 5 and hobbing lands in the DIN 7–8 band. Where a drawing sits inside that range decides the route and the price; where it sits outside it, we say so before quoting rather than after.
A drawing that mixes two systems without stating the conversion basis is a drawing that will be argued about at inspection. AGMA conversion in particular is approximate and depends on module and diameter, so the conversion basis belongs on the drawing.
Material and heat treatment
The drawing normally states the steel grade and the heat treatment. Where it leaves them open we raise the question rather than assume a default: the same tooth geometry in two different steels behaves differently in service, and the choice belongs to the design, not to the workshop.
The combinations that come up most often:
| Steel | Typical treatment | Resulting hardness | Where it is used |
|---|---|---|---|
| 40Cr | Quench and temper | HB 260–300 | Low/medium speed, moderate load, machine-tool gears, general reducers |
| 42CrMo | Quench and temper | HB 280–320 | Large-module heavy shafts, large-diameter gears |
| 20CrMnTi | Carburize and quench | Surface HRC 58–62, core HRC 30–42 | Automotive transmissions, industrial reducer gears |
| 17CrNiMo6 | Carburize and quench | Surface HRC 58–62, core HRC 33–45 | Heavy-duty gearboxes, high-reverse duty |
| 38CrMoAl | Quench and temper, then nitride | Surface ~HV 950–1100, layer 0.3–0.6 mm | Small-module precision gears, tight distortion limits |
Two things are worth stating plainly. First, the hardness figure is a range, not a target value — a report showing 59 HRC on one tooth and 61 on another is normal for carburized work and is not a defect. Second, case depth carries as much of the load capacity as surface hardness does, and deeper is not automatically better: a deep case lengthens the cycle, adds distortion and adds cost, so the depth is set by the contact stress the design actually carries.
Inspection
Tooth measurement covers four deviations, and they are not interchangeable:
- Fp — total cumulative pitch deviation around the whole gear. Drives transmission error at low frequency.
- fpt — single pitch deviation. Affects load sharing between teeth.
- fα — profile form deviation. Governs how the tooth contacts along its height.
- fβ — helix (lead) deviation. Governs end-to-end contact along the face width, and is the most damaging of the four when it is out, because it concentrates load at one end of the tooth.
A gear can pass Fp and fail on fβ and still be unusable in a quiet drive. An inspection report listing one or two parameters is not a report — it is a summary.
Alongside the tooth parameters we check runout against the datum the drawing names, bore and keyway dimensions, and, for gear shafts, the alignment between the tooth and the bearing journals. Where the customer supplies a mating gear, the pair is checked for backlash at the stated centre distance.
Failure modes the design should anticipate
The failures that come back to a gear shop are rarely “the gear was soft”. They are:
- Pitting on the flank, from contact stress above what the surface can carry — usually a hardness or a load-rating question, not a machining one
- Scuffing, from oil film breakdown at high sliding speed — a lubrication and surface finish issue
- Tooth root cracking, from bending fatigue, often starting at a sharp fillet or a machining mark in the root
- End loading, from helix deviation or misalignment, showing as wear concentrated at one end of the face
- Noise without visible wear, from pitch or runout error — the one that is a machining question from the start
What we need in order to quote
- The drawing as PDF, DXF or STEP
- Quantity, and whether it repeats
- The mating gear or pinion drawing, where backlash and centre distance matter
- Any requirement on marking, packing or documentation
If the drawing is still being finalized, send it with the open items marked. A quote built on a stated assumption is more useful than a quote that waits for the drawing to be perfect.